Welding & Soldering
MIG, TIG, stick consumables, torches, filler and solder.
Also searched as: welding wiretigmigwelding rodsolderflux
-
Soldering Iron
Power: 60W
-
Soldering Iron Gun
Power: 65WVoltage: 110V
-
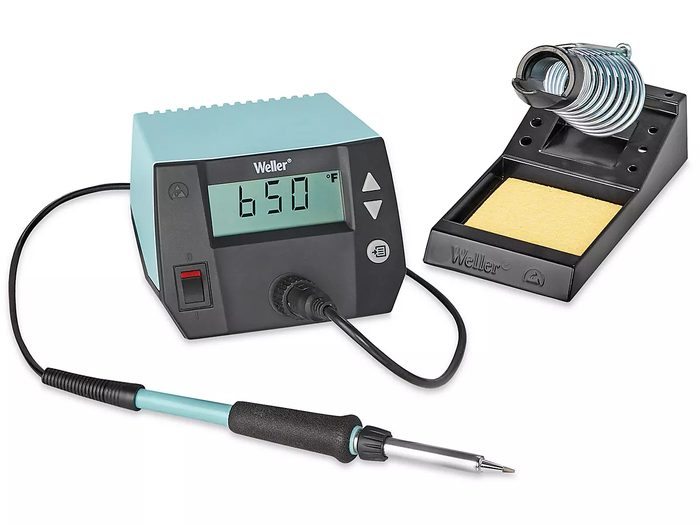
Soldering Iron Kit
Display: LCD DigitalPower: 80WVoltage: 110V
-
Soldering Iron Kit
Power: 60W
-
-
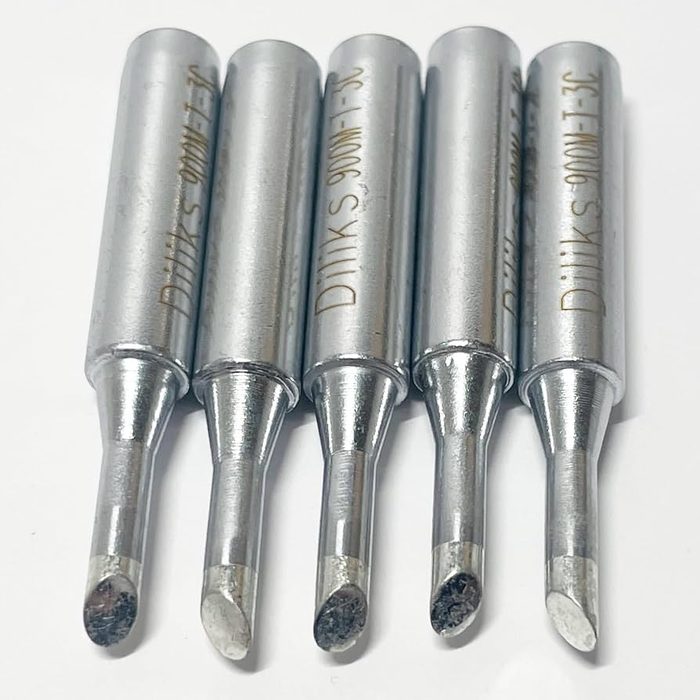
Soldering Tip, 900M-T-S3
Maximum Operating Temperature: 850 Degrees FTip Length: 18 mmTip Type: ChiselTip Width: 13/64 in
-
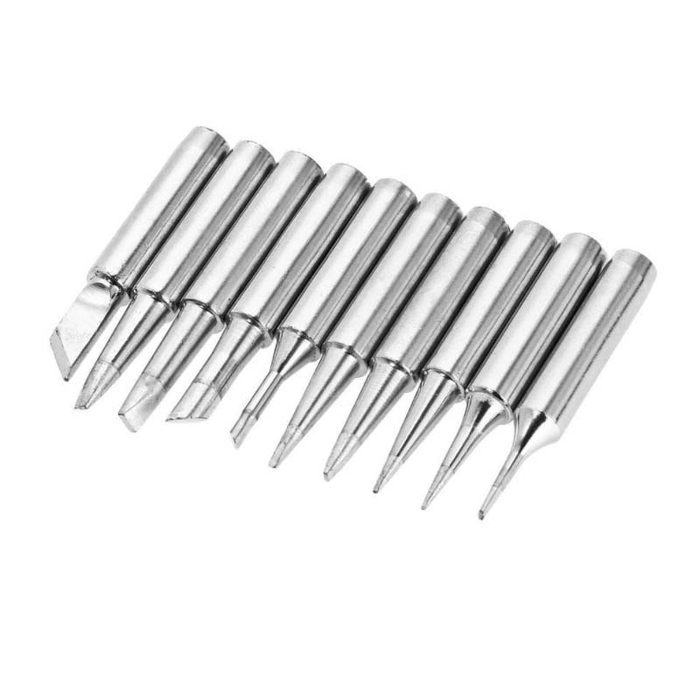
Soldering Tip, Chisel
Maximum Operating Temperature: 850 Degrees FTip Length: 19 mmTip Series: RTTip Type: ChiselTip Width: 3.6 mm
-
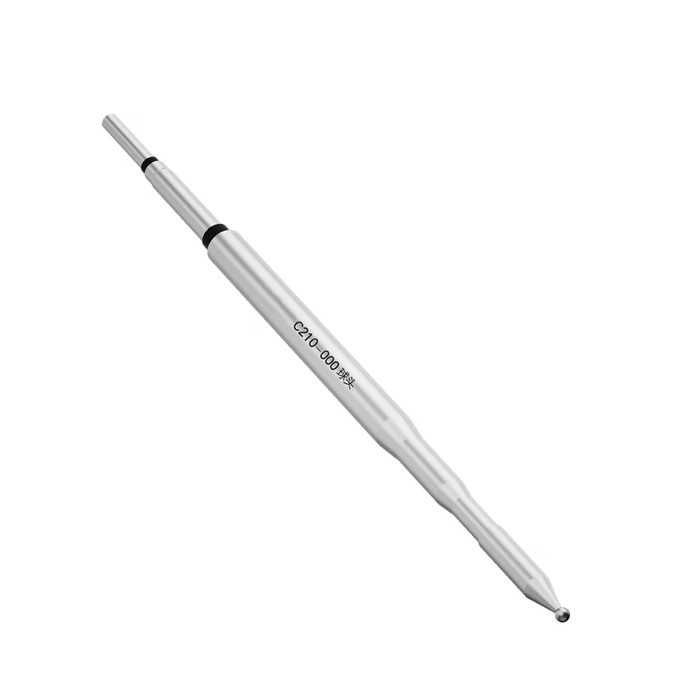
Spherical Solder Tip
Diameter: 1 mm
-
-
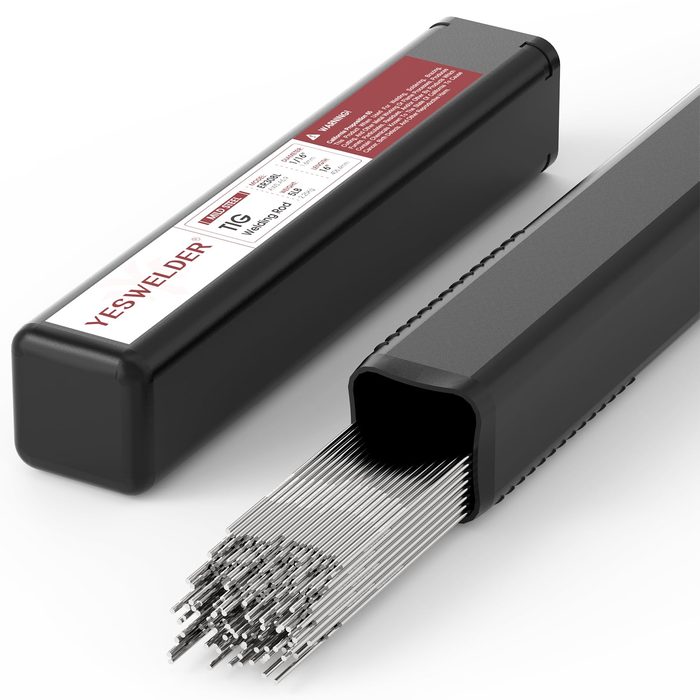
Stainless Steel TIG Welding Rod
Diameter: 1/16"Length: 36"Quantity: 10
-
 from $2.20Made-in-China $2.20
-
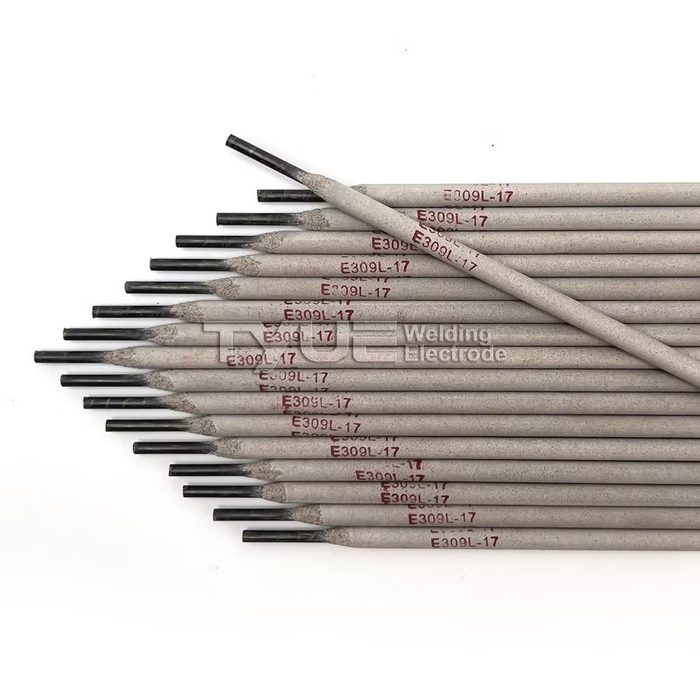
Stick Welding Electrode
Diameter: 1/2 inchLength: 12 inchRod Shape: Round
-
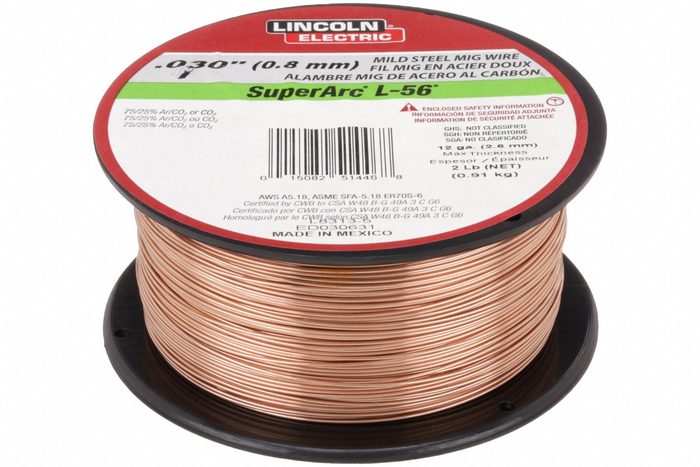
SuperArc L-56 ER70S-6 MIG Welding Wire
Diameter: 0.025 in.
-
SuperArc L-56 ER70S-6 MIG Welding Wire
Diameter: 0.030 in.Weight: 2 lb.
-
SuperArc L-56 ER70S-6 MIG Welding Wire for Mild Steel
Diameter: 0.035 inWeight: 12.5 lb
-
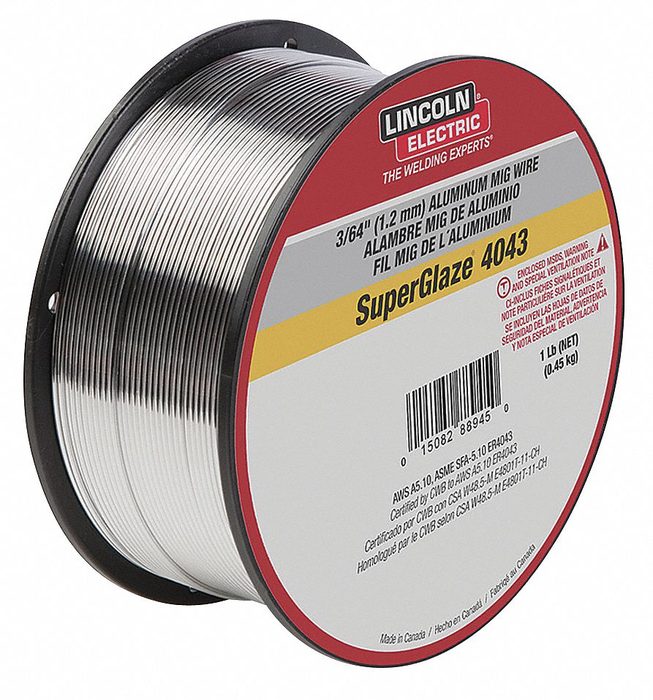
Superglaze ER4043 Aluminum MIG Welding Wire
Diameter: 0.030 in.Weight: 1 lb.
-
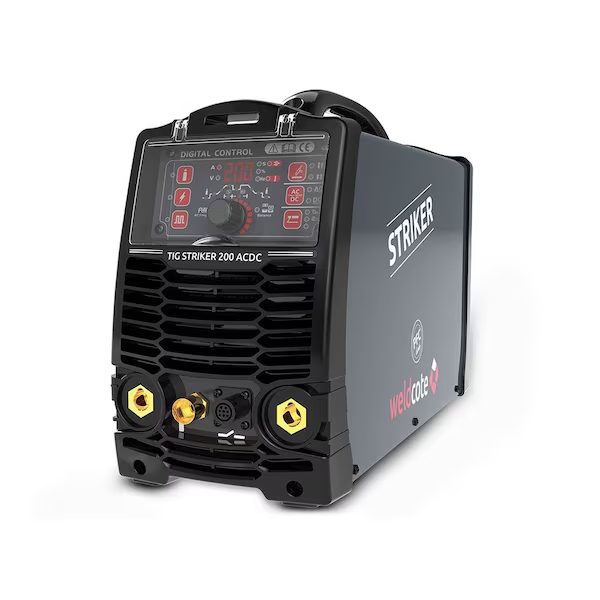
TIG 200 Welding Machine
Amperage: 200 ATechnology: PWM, IGBT
-
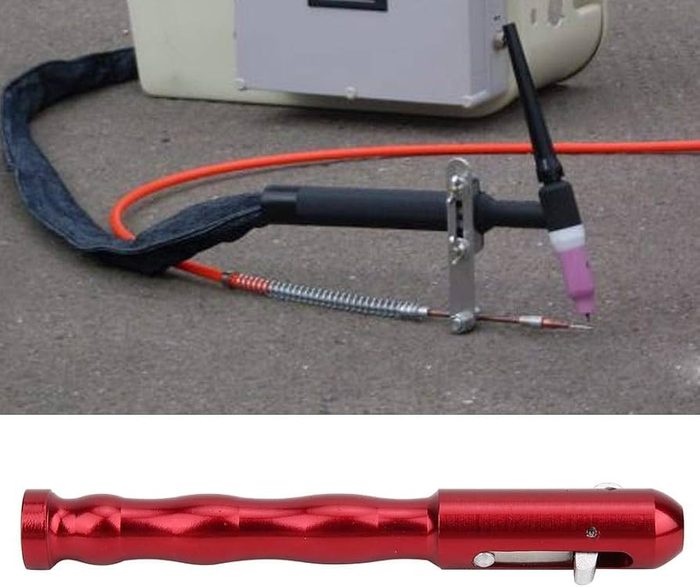
TIG Finger Feeder PW1550
Rod Diameter Range: 0.030" to 0.125"
-
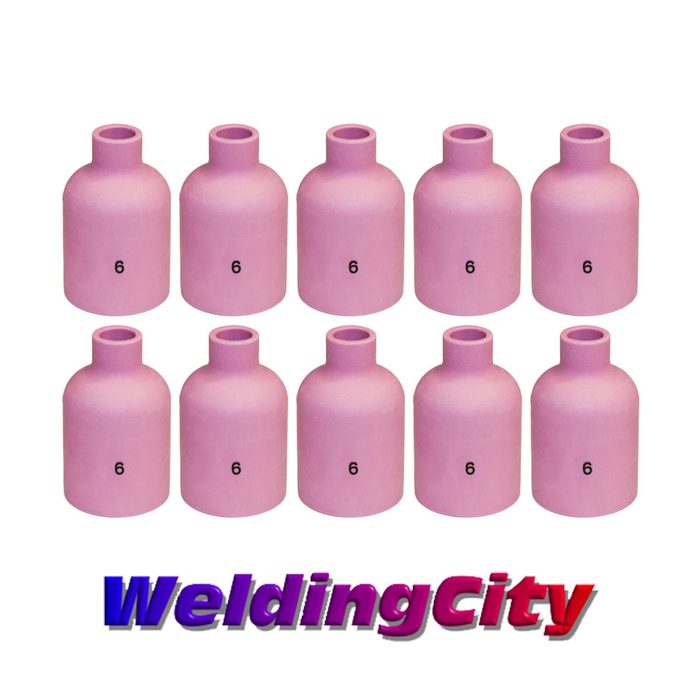
TIG Large Gas Lens
Torch Series Compatibility: TIG 17, 18, 26Tungsten Electrode Diameter: 3/32"
-
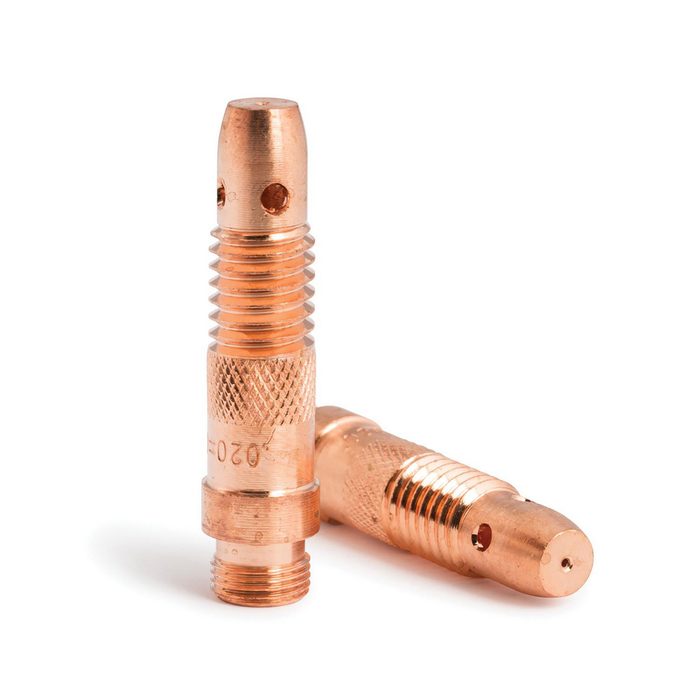
TIG Torch Collet Body, 0.0200" Hole Diameter, Copper Alloy
For Use With: 9/20 TIG TorchesHole Diameter: 0.0200"Product Type: Collet Body
-
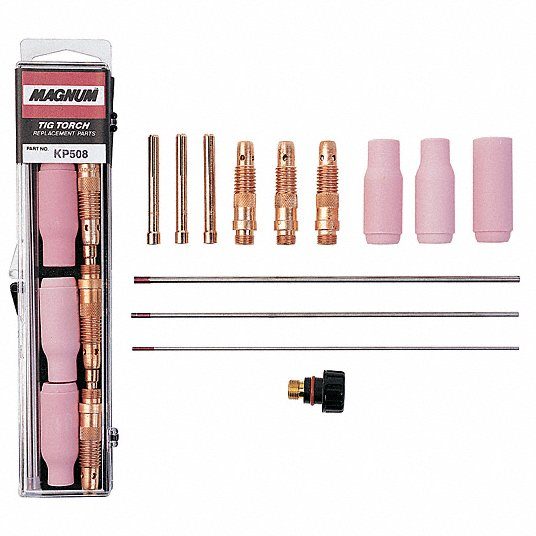
TIG Torch Expendable Parts Kit for 17/18/26 Series TIG Torches
For Use With: 17/18/26 Series TIG Torches
-
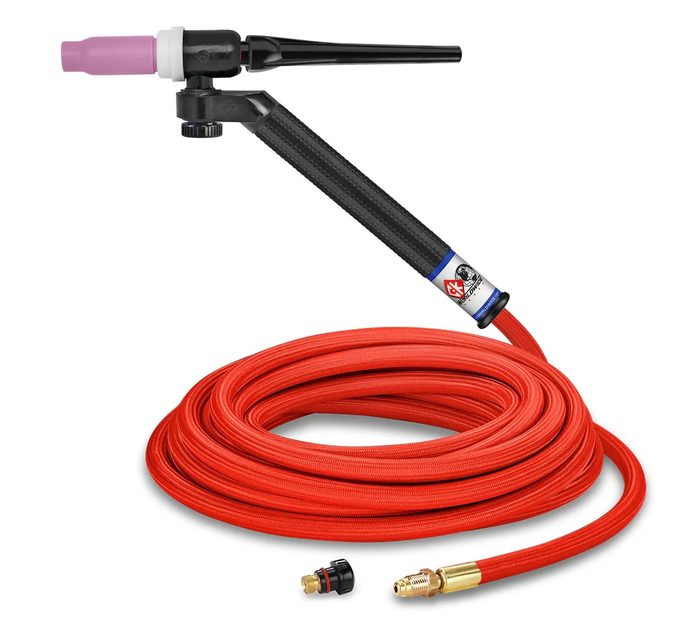
TIG Torch, 17 Series
Length: 12 ftTorch Series: 17
-
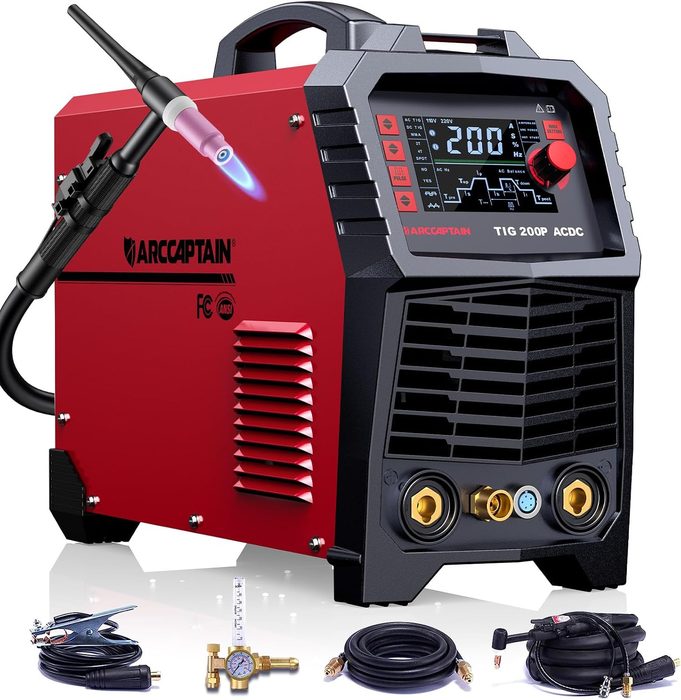
TIG Welder
Amperage: 200AVoltage: 110V
-
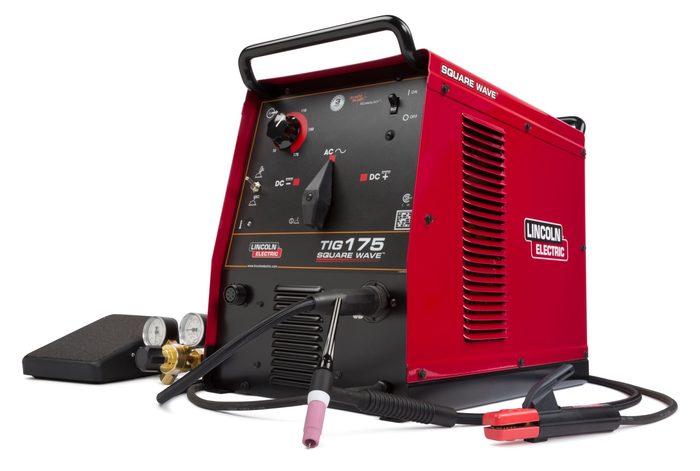
TIG Welder
Voltage: 208/230/460V
-
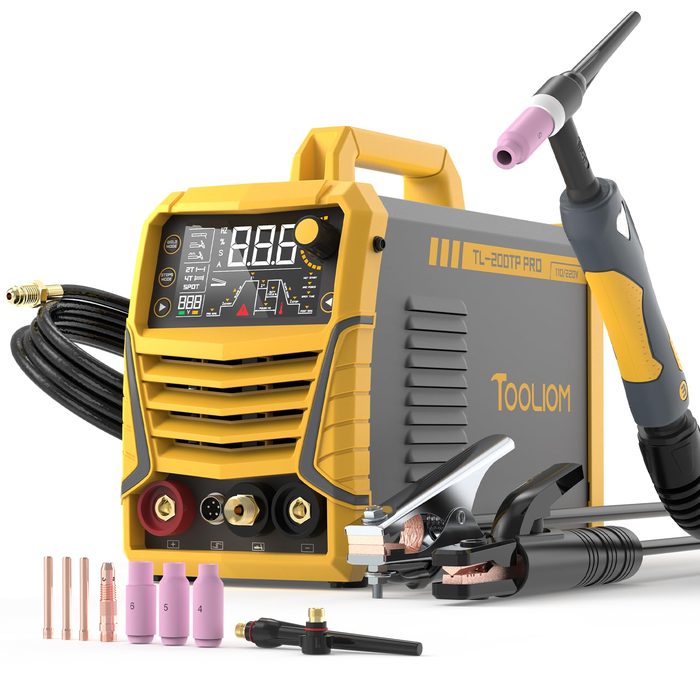
TIG Welder
Voltage: 34 V
-
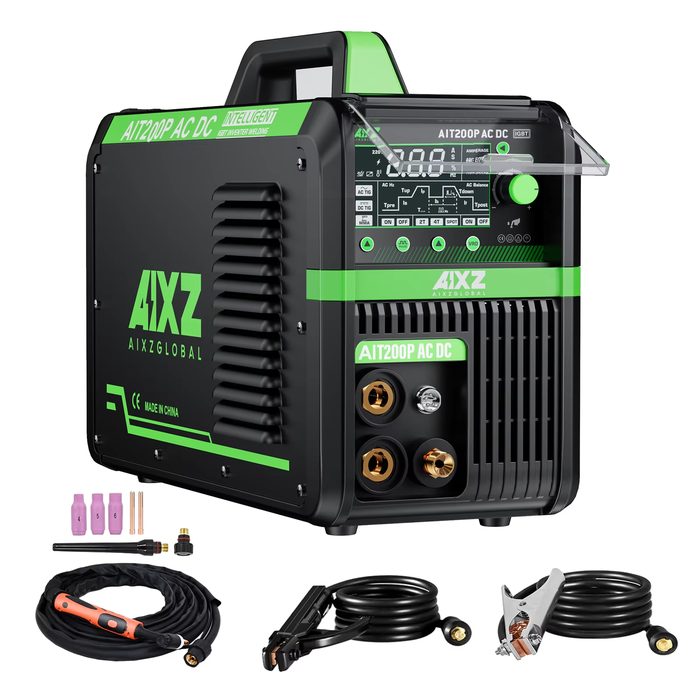
TIG Welder Laser Welding Machine
Control Mode: ManualProcess: TIG LaserVoltage: AC220V
-
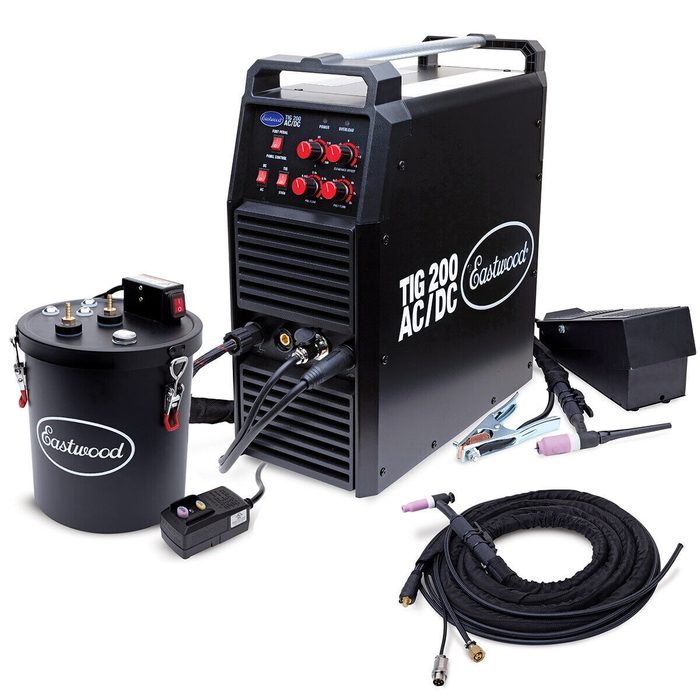
TIG Welder and Stick Welder
Amperage: 220 AMP
-
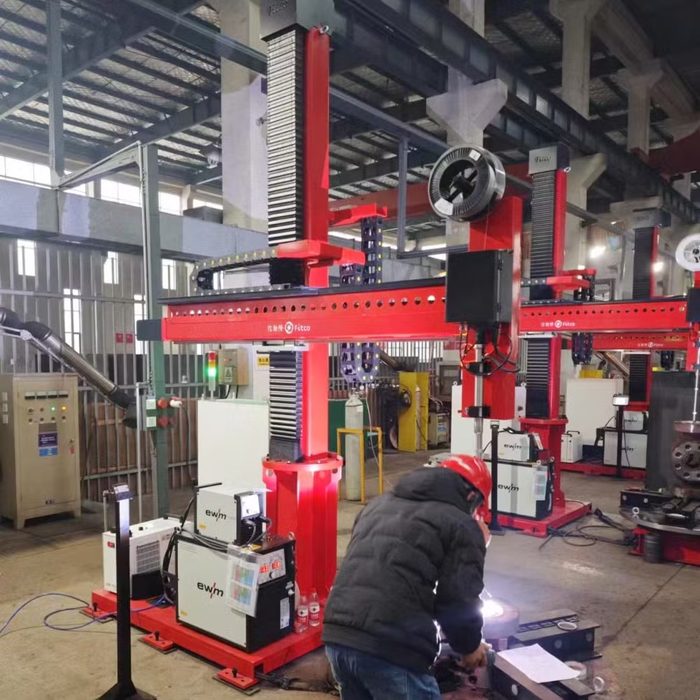
TIG Welding Cladding Station
Process: TIG
-
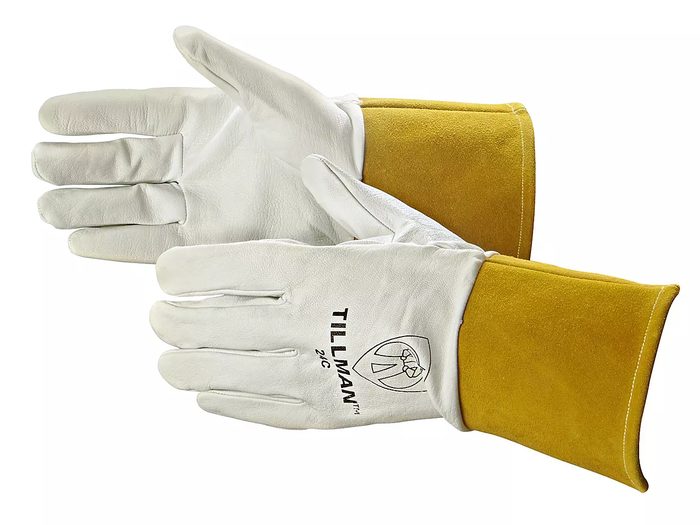
TIG Welding Gloves
Cuff Length: 4"Overall Length: 11.25"
-
TIG Welding Gloves - Medium
Size: Medium
-
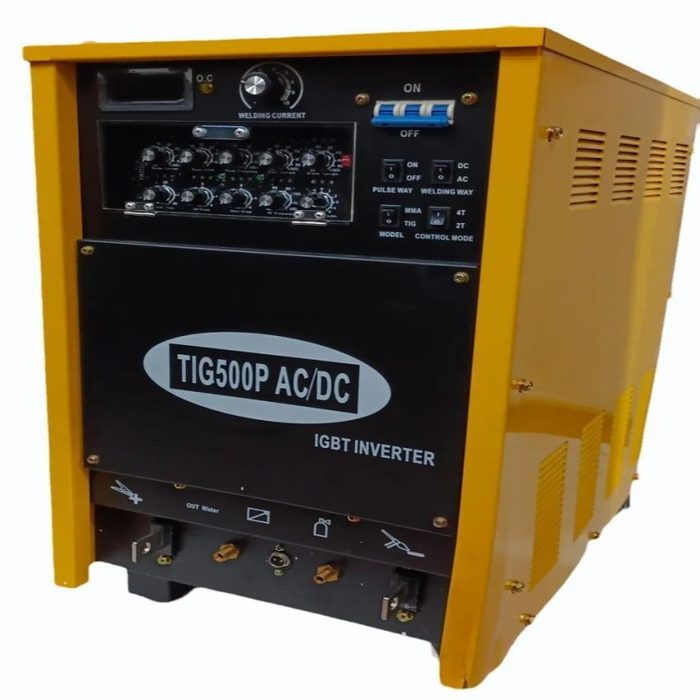
TIG Welding Machine
Cooling Way: Water/Air CoolingFrequency Range: Low FrequencyStyle: Hanging
-
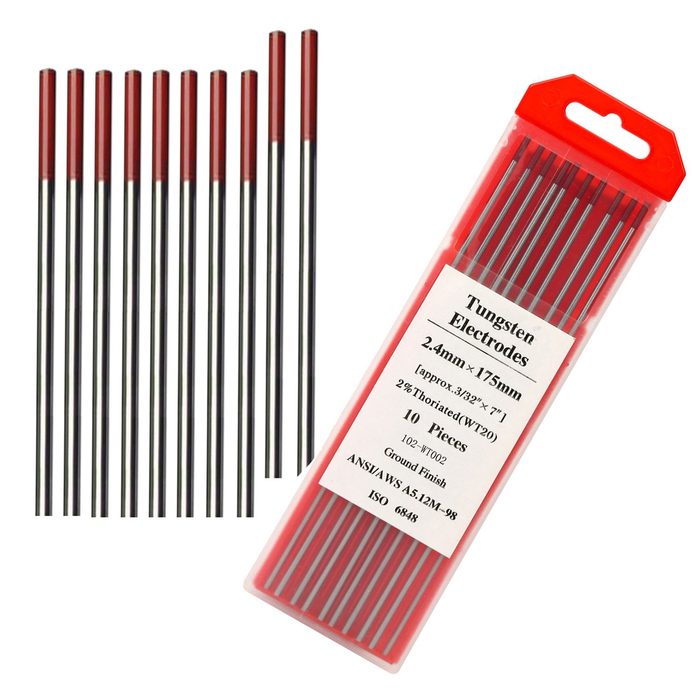
TIG Welding Rod
Diameter: 0.094 inchOverall Length: 36 inch
-
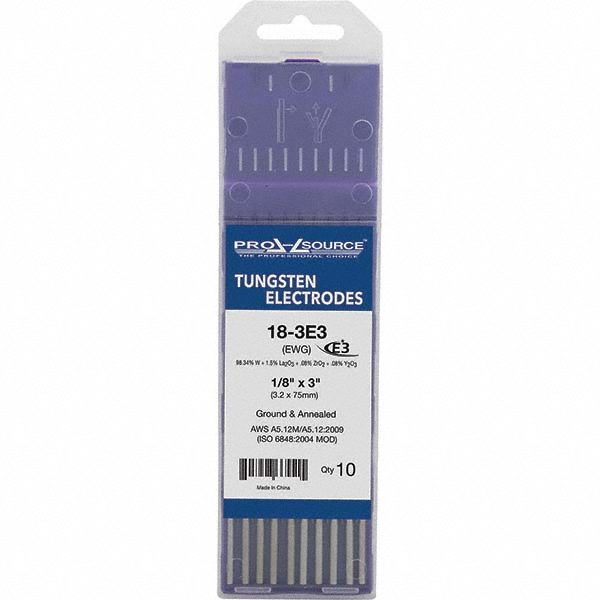
TIG Welding Rod E3
Color Code: PurpleDiameter: 1/16 inchOverall Length: 3 inch
-
TIG Welding Rod, 3/32" Dia
Diameter: 3/32 in
-
TIG Welding Rod, Flux Coated
Diameter: 1/8 inchLength: 36 inch
-
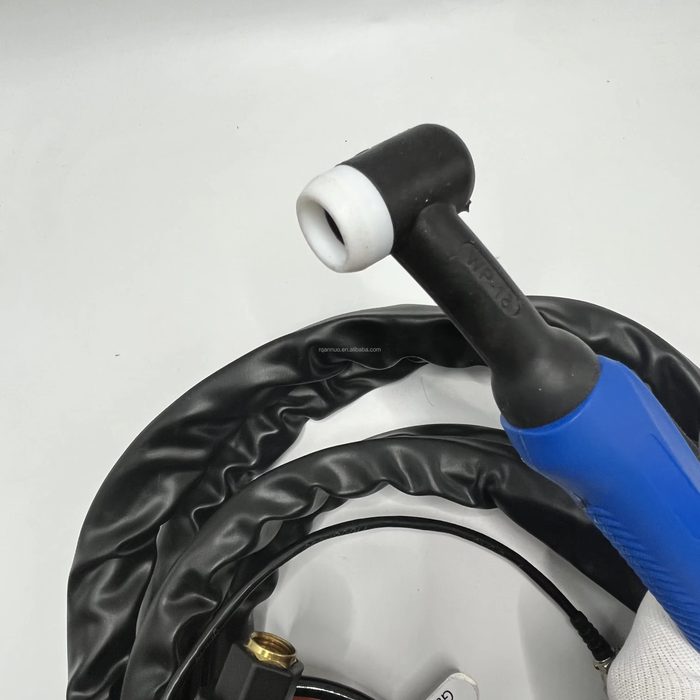
TIG Welding Torch, Water Cooled, 350 A, 0.75' Cable, Silicone Rubber Body
Amperage: 350 ABody Material: Silicone RubberCable Length: 0.75'Cooling: Water Cooled
About welding & soldering
Welding and soldering consumables encompass a range of materials essential for joining metals through heat. MIG (Gas Metal Arc Welding) consumables include solid wires, flux-cored wires, and shielding gases such as argon, CO2, or argon/CO2 blends. Wire diameters typically range from 0.023" to 0.062" (0.6mm to 1.6mm), with common alloys like ER70S-6 for mild steel, ER308L for stainless steel, and ER5356 for aluminum. TIG (Gas Tungsten Arc Welding) requires non-consumable tungsten electrodes, typically pure, thoriated, ceriated, or lanthanated, with diameters from 0.020" to 0.250" (0.5mm to 6.4mm). Filler rods, available in similar alloys to MIG wires, are fed manually. Stick welding (Shielded Metal Arc Welding) utilizes flux-coated electrodes, classified by AWS standards (e.g., E6010, E7018), indicating tensile strength, position capabilities, and coating type. Solder, used for lower-temperature joining, commonly consists of tin-lead (e.g., Sn60Pb40) or lead-free alloys (e.g., Sn96.5Ag3.0Cu0.5). Flux, either liquid or paste, is critical for cleaning surfaces and preventing oxidation during both soldering and brazing processes. Torches, for both MIG and TIG, are selected based on amperage rating, cooling method (air or water), and ergonomic considerations, with various nozzle and collet body sizes available to accommodate different electrode and wire diameters.
How to choose
Selecting welding and soldering consumables begins with the joining process: MIG, TIG, stick, or soldering. This dictates the primary consumable type. Next, identify the base material to be joined (e.g., mild steel, stainless steel, aluminum, copper) to determine the appropriate filler metal alloy or solder composition. Consider the required mechanical properties of the joint, such as tensile strength, which influences electrode classification (e.g., E7018 vs. E6010) or filler wire alloy. For welding, evaluate the joint configuration and position, as some consumables are position-specific. Finally, match the consumable dimensions (wire diameter, electrode size, solder gauge) to the equipment's capabilities and the desired deposition rate or joint size, ensuring proper fit and performance.